-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

2026 Best Carbon Seamless Pipe Manufacturer Guide
Choosing the right Carbon Seamless Pipe Manufacturer requires more than comparing prices or polished websites. Material traceability matters.
The World Steel Association reported approximately 1.88 billion tonnes of crude steel production in 2024. The International Energy Agency also notes that steelmaking creates roughly 7% to 9% of global energy-related emissions. These figures reveal the industry’s scale, cost pressure, and environmental responsibility. A serious manufacturer must therefore control chemistry, furnace conditions, piercing, heat treatment, and inspection.
Quality begins inside the mill.
This 2026 guide evaluates manufacturers through practical evidence. Important indicators include ISO 9001 systems, API 5L capability, ASTM compliance, ultrasonic testing, hydrostatic testing, and complete mill test certificates. Production capacity also matters, but capacity alone proves little. A small facility with disciplined inspection may outperform a larger supplier with weak documentation.
As steel industry leader Lakshmi Mittal has said, “Steel is the backbone of modern society.” That backbone must withstand pressure, corrosion, vibration, and demanding service conditions. Buyers should inspect sample reports, verify third-party certificates, and request photographs of markings, bundles, and warehouse storage. A reliable Carbon Seamless Pipe Manufacturer should explain tolerances clearly, not hide behind vague claims.
No ranking is perfect.
Market data can lag behind factory changes. Supplier performance can also vary by batch, destination, and specification. This guide recognizes that limitation. It focuses on verifiable experience, technical knowledge, transparent communication, and independent evidence. Those details help engineers, distributors, and project buyers make safer decisions in 2026.
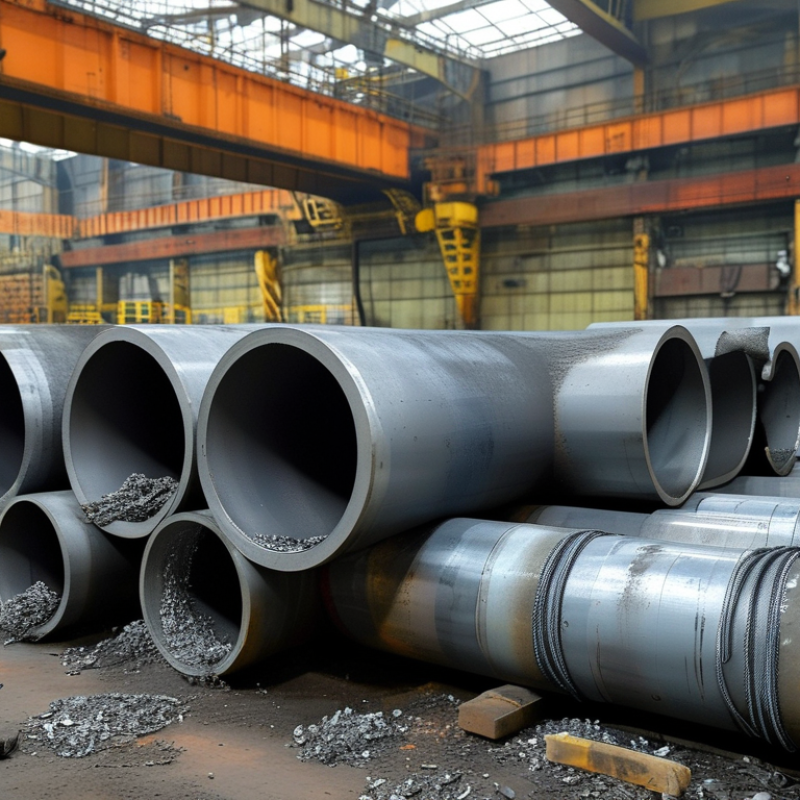
Table of Contents [Hide]
Carbon Seamless Pipe Basics: Grades, Sizes, and ASTM A106 Requirements
Carbon seamless pipe is selected for pressure, temperature, and corrosion conditions. ASTM A106 covers seamless carbon steel pipe for high-temperature service. It is commonly specified in Grades A, B, and C. Grade B is widely used because it balances strength, weldability, and cost. Grade C offers higher strength, but the project design must justify it.
Sizes normally follow nominal pipe size and schedule. The schedule controls wall thickness, not the outside diameter. For example, NPS 2 Schedule 40 and Schedule 80 share the same nominal diameter. Their pressure capacity and weight differ. Inspectors should verify outside diameter, wall thickness, straightness, end preparation, and heat numbers. Small details matter.
ASTM A106 requires chemical and mechanical compliance, along with defined testing and dimensional tolerances. Tensile strength, yield strength, elongation, and hydrostatic testing are important acceptance points. Mill certificates should match the pipe markings and purchase specification. In demanding service, additional nondestructive examination may be requested by the buyer. However, A106 alone does not guarantee suitability for every fluid or temperature. A neat certificate cannot replace engineering review. Some specifications are also misunderstood, especially when schedule is treated as a complete design decision. Temperature cycling, welding procedures, and corrosion allowance still need careful evaluation.
2026 Best Carbon Seamless Pipe Manufacturer Guide - Carbon Seamless Pipe Basics: Grades, Sizes, and ASTM A106 Requirements
| Data Category | Item or Requirement | Typical Data / Standard Requirement | Practical Notes |
|---|---|---|---|
| Product Type | Carbon steel seamless pipe | Manufactured without a welded longitudinal seam; commonly produced by hot working and, for some sizes, cold finishing. | Used for pressure piping, process services, steam lines, water lines, and elevated-temperature applications. |
| Primary Material Standard | ASTM A106 / A106M | Seamless carbon steel pipe for high-temperature service. | The purchase order should identify the edition of the standard, grade, size, schedule or wall thickness, length, and inspection requirements. |
| Common Grades | Grade A, Grade B, Grade C | Grade B is widely selected for general industrial pressure piping; Grades A and C are chosen according to the required mechanical properties and design conditions. | Grade selection must be confirmed against the design code, operating temperature, pressure, corrosion conditions, and required weldability. |
| Carbon Content, Maximum | ASTM A106 chemical requirement | Grade A: 0.25%; Grade B: 0.30%; Grade C: 0.35%. | Values are percent by mass and should be verified using the material test certificate. |
| Manganese | ASTM A106 chemical requirement | Grade A: 0.27–0.93%; Grade B: 0.29–1.06%; Grade C: 0.29–1.06%. | The actual heat analysis may vary within the limits specified by the applicable ASTM edition. |
| Silicon | ASTM A106 chemical requirement | Minimum 0.10% for Grades A, B, and C. | Silicon supports deoxidation during steelmaking; certificate values should be checked for each heat. |
| Phosphorus and Sulfur | ASTM A106 chemical limits | Phosphorus: 0.035% maximum; Sulfur: 0.035% maximum. | Lower residual elements can be important for weldability and fracture-related requirements, subject to the project specification. |
| Tensile Strength, Minimum | ASTM A106 mechanical requirement | Grade A: 48 ksi (330 MPa); Grade B: 60 ksi (415 MPa); Grade C: 70 ksi (485 MPa). | Metric conversions are approximate; the governing standard should be used for compliance decisions. |
| Yield Strength, Minimum | ASTM A106 mechanical requirement | Grade A: 30 ksi (205 MPa); Grade B: 35 ksi (240 MPa); Grade C: 40 ksi (275 MPa). | Design allowable stress is not the same as minimum yield strength and must be taken from the applicable design code. |
| Standard Outside-Diameter Range | Nominal pipe size selection | ASTM A106 commonly covers NPS 1/8 through NPS 48, subject to product availability and the applicable dimensional specification. | Large-diameter orders should confirm manufacturing capability, wall-thickness range, length, and inspection scope before purchase. |
| Dimensional Reference | ASME B36.10M | Provides standard outside diameters and nominal wall thicknesses for welded and seamless wrought steel pipe. | ASTM A106 defines material and product requirements; ASME B36.10M is commonly used to identify nominal dimensions. |
| NPS 1/2 Example | Nominal size and schedule | Outside diameter: 0.840 in (21.3 mm); Schedule 40 wall: 0.109 in (2.77 mm); Schedule 80 wall: 0.147 in (3.73 mm); Schedule 160 wall: 0.187 in (4.78 mm). | Actual inside diameter is approximately outside diameter minus twice the nominal wall thickness, before tolerance considerations. |
| NPS 2 Example | Nominal size and schedule | Outside diameter: 2.375 in (60.3 mm); Schedule 40 wall: 0.154 in (3.91 mm); Schedule 80 wall: 0.218 in (5.54 mm); Schedule 160 wall: 0.343 in (8.74 mm). | NPS is a nominal designation; it does not always equal the measured outside diameter in inches. |
| NPS 4 Example | Nominal size and schedule | Outside diameter: 4.500 in (114.3 mm); Schedule 40 wall: 0.237 in (6.02 mm); Schedule 80 wall: 0.337 in (8.56 mm); Schedule 160 wall: 0.531 in (13.49 mm). | Use the project piping class to confirm the required schedule, corrosion allowance, and pressure-temperature rating. |
| NPS 8 Example | Nominal size and schedule | Outside diameter: 8.625 in (219.1 mm); Schedule 40 wall: 0.322 in (8.18 mm); Schedule 80 wall: 0.500 in (12.70 mm); Schedule 160 wall: 0.906 in (23.01 mm). | Heavy-wall pipe may require special handling, beveling, welding procedures, and dimensional checks. |
| NPS 12 Example | Nominal size and schedule | Outside diameter: 12.750 in (323.9 mm); Schedule 40 wall: 0.375 in (9.53 mm); Schedule 80 wall: 0.500 in (12.70 mm); Schedule 160 wall: 1.312 in (33.32 mm). | For large sizes, verify whether the specified wall thickness is standard, special, or project-specific. |
| Length Options | Commercial supply lengths | Random lengths are commonly supplied; exact-length, double-random, and cut-length requirements may be specified by the purchaser. | Length tolerances and end conditions should be stated in the purchase specification. |
| End Finishes | Plain, beveled, or threaded ends | Plain ends are common for fabrication; beveled ends are used for butt welding; threaded ends are used where permitted by the piping design. | End preparation must match the welding procedure, fitting type, or connection standard. |
| Heat Treatment | ASTM A106 processing requirement | Hot-finished pipe is generally supplied without mandatory heat treatment unless required by the specification; cold-drawn pipe is heat treated after the final cold-drawing operation. | Confirm the required delivery condition and any additional post-weld heat-treatment requirements with the design code. |
| Hydrostatic Test | ASTM A106 test requirement | Each length is normally subjected to a hydrostatic test unless an approved nondestructive electric test option is specified. | Test pressure, holding time, and acceptance criteria should be verified against the applicable ASTM edition and purchase order. |
| Inspection Documents | Material Test Report | A typical report includes heat number, chemical analysis, tensile and yield results, elongation, hydrostatic or nondestructive test status, dimensions, and standard compliance. | Traceability markings should remain identifiable during cutting, fabrication, and installation. |
| Selection Checklist | Key information for purchasing | Specify ASTM A106/A106M, grade, NPS or outside diameter, schedule or wall thickness, length, end finish, quantity, testing, coating or preservation, and documentation. | Final acceptance should be based on the latest applicable standard, approved drawings, piping class, and project quality plan. |
Note: Dimensions shown in the examples are nominal values commonly referenced from ASME B36.10M. Always verify the applicable ASTM A106/A106M edition, ASME dimensional standard, design code, and purchase specification before fabrication or installation.