-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

7 Tips for Buying Aluminized Steel Coil?
Buying Aluminized Steel Coil is not simply a price comparison. It is a performance decision involving heat, corrosion, forming, and service life. World Steel Association data recorded approximately 1.89 billion tonnes of crude steel production in 2023. That scale creates many suppliers, grades, and quality differences. Buyers need evidence, not attractive photographs.
ASTM A463/A463M provides the main specification for aluminum-coated steel sheet. It addresses coating type, steel grade, thickness, and mechanical requirements. The IEA reports that iron and steel production contributes roughly 7% to 9% of global energy-related carbon dioxide emissions. Responsible sourcing therefore matters. Dr. S. M. A. Shibli, a researcher in coated-steel corrosion, states, “The coating–substrate interface strongly influences aluminized steel performance.” That detail is easy to overlook.
This guide presents seven practical buying tips. It examines coating mass, base-steel grade, coil thickness, width tolerance, surface condition, testing documents, and supplier reliability. Ask for the mill test certificate. Check the coating designation. Confirm whether the coil suits stamping, bending, welding, or high-temperature service. A bright surface can still hide poor adhesion. The cheapest offer may become expensive after cracking, trimming losses, or early corrosion. A perfect checklist does not exist. Buyers must still question unclear data, compare samples, and inspect the actual coil edges. These small actions support safer decisions and more consistent production results.
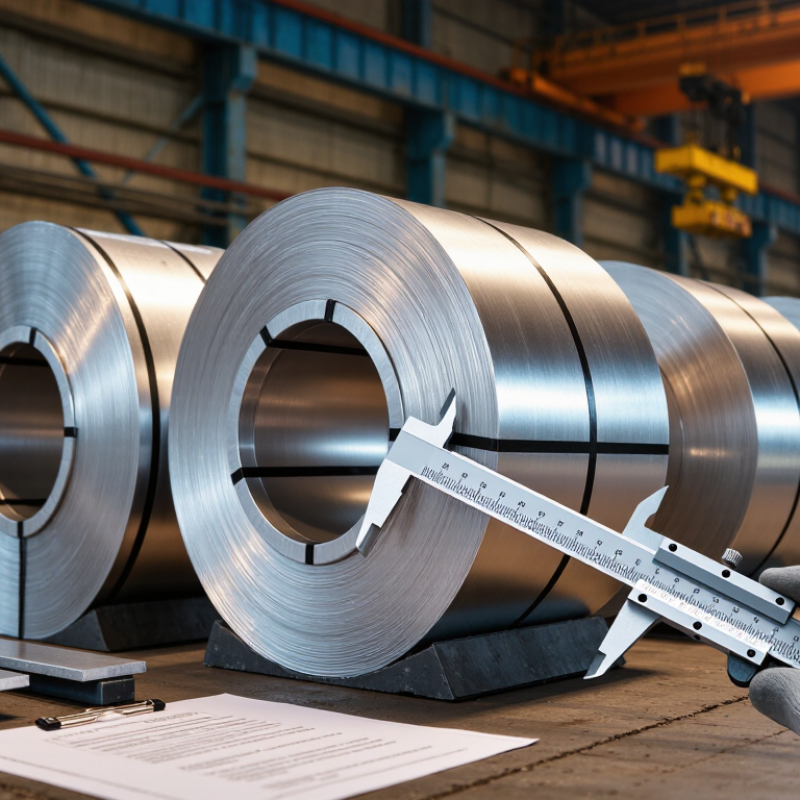
Table of Contents [Hide]
Define the Performance Requirements for Aluminized Steel Coil
7 Tips for Buying Aluminized Steel Coil: Define the Performance Requirements
Performance requirements should come before price, thickness, or delivery terms. Identify the service temperature, corrosion exposure, forming method, and expected operating life. ASTM A463/A463M covers aluminum-coated carbon steel sheet and defines coating classes, including approximate total coating masses from 75 to 183 g/m² for T1 through T3 grades. More coating is not automatically better. It may affect forming, welding, and cost.
Specify the substrate strength and thickness tolerance clearly. For exhaust ducts, heat shields, or industrial panels, continuous exposure temperature matters. For outdoor storage tanks, use ISO 9223 atmospheric corrosivity categories, ranging from C1 to CX, to describe the environment. Salt spray, condensation, sulfur compounds, and trapped moisture can change the selection. Ask for coating mass test results, tensile data, bend-test performance, and heat-resistance evidence. Request the actual mill certificate.
Watch the details.
In practical purchasing reviews, many failures begin with vague terms like “high corrosion resistance.” That phrase cannot replace a defined coating class or test condition. Confirm whether the quoted coating mass applies to both surfaces and which test method was used. A neat specification can still be wrong. I would also include a small forming trial before approving a large order, because laboratory data may not reflect sharp bends, damaged edges, or production handling. Sources: ASTM A463/A463M and ISO 9223.