-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

What Is the Best GRP Gutter Machinery in 2026?
Choosing the best Grp Gutters Machinery in 2026 requires more than comparing prices or brochure speeds. A reliable system must produce straight, clean gutter profiles with consistent wall thickness. It should also manage resin distribution, curing conditions, pulling force, and cutting accuracy. Small errors become visible on a finished roof. Warped edges are expensive to correct.
Michael Turner, a GRP production engineer with experience in composite profile manufacturing, says, “The best machine is the one that keeps quality stable during a full production shift.” That point matters. A machine may perform well during a short demonstration, yet struggle after hours of continuous operation. Buyers should inspect the forming die, heating zones, resin delivery system, puller, cutter, and control panel. Maintenance access deserves attention too. Dust, cured resin, and fibre fragments quickly collect around moving parts.
Look closely.
The strongest Grp Gutters Machinery combines accurate forming with practical service support. Automatic controls can reduce operator variation, but they cannot replace skilled supervision. Energy use, changeover time, spare-part availability, and training should influence the decision. A lower purchase price may create higher long-term costs. This is easy to overlook.
There is no universal winner. A small workshop may need a compact, flexible line. A large manufacturer may prefer higher output and automated handling. The best choice depends on gutter dimensions, daily volume, labour experience, and product standards. Even this approach has limits. Supplier claims should be tested against samples, production records, and references from comparable factories. That evidence gives the final decision greater credibility.
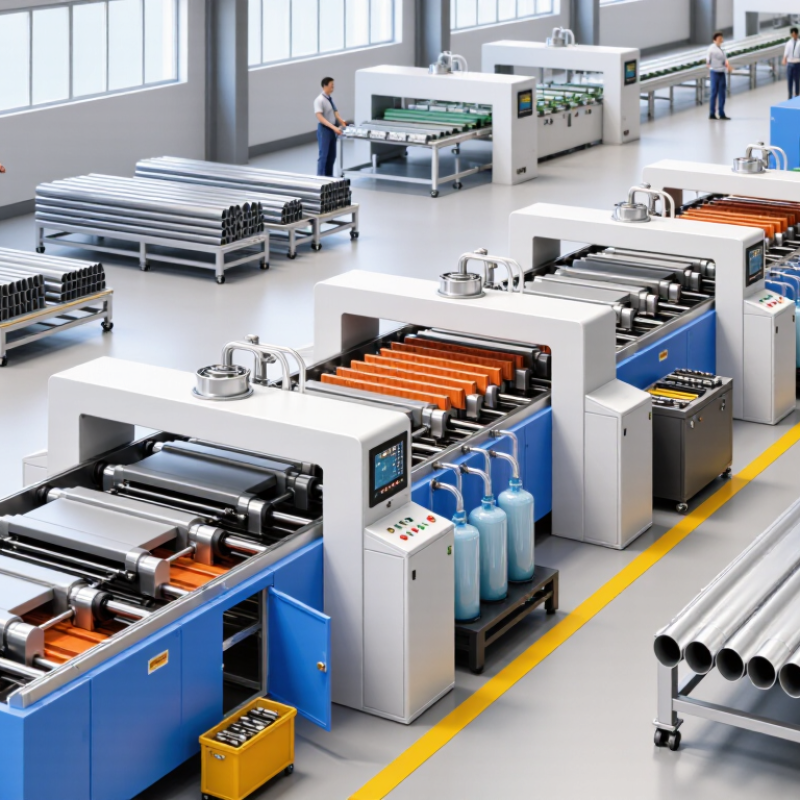
Table of Contents [Hide]
GRP Gutter Machinery Explained: Pultrusion, Resin, and Cutting Units
Choosing the best GRP gutter machinery in 2026 starts with understanding the complete production line. Pultrusion equipment pulls glass fibres through a resin bath and heated forming die. This creates consistent profiles with strong, lightweight reinforcement. Stable pulling speed matters. Small speed changes can affect thickness, surface quality, and curing.
The resin unit controls the mixture entering the fibre package. Accurate metering reduces dry spots, air pockets, and unnecessary resin waste. Operators should check viscosity, temperature, and fibre wet-out during each shift. A clean tank helps. Resin systems vary, so one setting may not suit every profile or climate. I have seen production teams trust automatic readings too quickly. Manual checks still reveal problems that sensors sometimes miss.
Cutting units finish the profile after curing. A reliable saw should produce square ends without crushing the laminate. Adjustable guides support different gutter sizes, while dust extraction protects the work area and improves visibility. Cutting speed must match the cured profile and blade condition. Poor alignment creates fitting problems at installation sites. The best setup is not always the fastest one. It balances output, repeatability, maintenance access, and operator control. Even well-designed machinery needs regular calibration, because wear gradually changes real production results.