-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

China Best Copper Busbar Extrusion Machine Supplier?
The global shift toward electrification is making copper processing capacity more important. The International Energy Agency reported in its Global Critical Minerals Outlook 2024 that copper demand will rise sharply through 2035, driven by power grids, electric vehicles, and renewable energy. The International Copper Association also identifies electrical applications as copper’s largest demand segment.
This pressure reaches the factory floor. A Copper Busbar Extrusion Machine must produce accurate profiles, stable surfaces, and consistent conductivity. Even a small dimensional error can create problems during switchgear assembly. Operators watch billet temperature, extrusion speed, die wear, and cooling conditions closely. The process looks straightforward. It is not.
Dr. Michael Widmer, metals strategist at Bank of America, has described copper as “the new oil,” highlighting its strategic role in modern infrastructure. His comment is broad, but it reflects a practical concern for equipment buyers: reliable copper output now affects project schedules and energy-system costs. S&P Global’s report, The Future of Copper, also warns that supply growth may struggle to match long-term demand. That gap makes machine selection more than a price comparison.
A capable Copper Busbar Extrusion Machine can reduce scrap, improve repeatability, and support larger production volumes. Yet no machine solves every production weakness. Poor rod quality, unsuitable tooling, or weak maintenance can still reduce performance. Buyers should examine verified output data, energy consumption, service response, and sample profiles before choosing a supplier. The best decision is rarely the cheapest one.
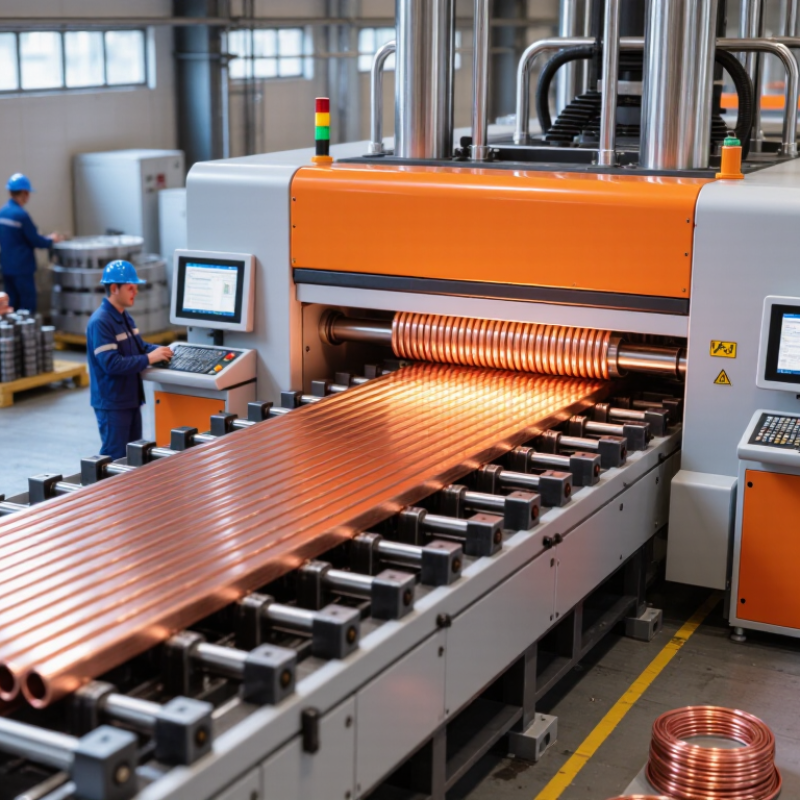
Table of Contents [Hide]
Copper Busbar Extrusion: 99.9% Pure Copper and 100% IACS Conductivity
Copper Busbar Extrusion: 99.9% Pure Copper and 100% IACS Conductivity
Selecting the right copper busbar extrusion machine requires more than checking output speed. The machine must process 99.9% pure copper with stable pressure, temperature, and alignment. High-purity copper supports excellent electrical performance, but conductivity can change after extrusion. Heat, surface oxidation, impurities, and excessive deformation may reduce the final result. A reliable supplier should explain these risks clearly. They should also provide material certificates, dimensional records, and conductivity test data. In practical production, a smooth busbar surface matters. Small scratches can complicate plating, bending, and insulation. Precision is not optional.
Tips: Confirm conductivity at the actual finished condition, not only from the raw copper certificate. Ask for testing at 20°C, using the IACS reference method. Check sample dimensions, corner radius, cooling control, and die wear. Request a trial extrusion before placing a large order. It is a modest step.
The phrase “100% IACS conductivity” needs careful interpretation. It usually refers to annealed copper under defined testing conditions, not every extruded busbar. A strong machine design should control billet heating, extrusion speed, cooling, and straightening. These details protect the copper’s structure and reduce distortion. Experienced technical support can help adjust the process for different widths and thicknesses. Still, no supplier should promise perfect results without testing. That promise sounds attractive, but it deserves questioning. A better evaluation compares measured samples, production consistency, energy use, and maintenance response.