-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

China Top Tungsten Alloy Manufacturer for Global Buyers?
Choosing a China Top Tungsten Alloy Manufacturer requires more than comparing prices on a supplier website. Global buyers often need stable density, accurate dimensions, clean surfaces, and dependable delivery. These details matter when tungsten alloy parts enter radiation shielding, aerospace counterweights, medical equipment, or precision tooling.
Materials expert W.-D. Schubert, co-author of Tungsten: Properties, Chemistry, Technology of the Element, Alloys, and Chemical Compounds, wrote, “Tungsten has the highest melting point of all metals.” That statement explains its value, but not the whole purchasing decision. A capable Tungsten Alloy Manufacturer must also control powder selection, sintering temperature, nickel-iron or nickel-copper bonding, machining tolerance, and final inspection. The material is difficult. Manufacturing is harder.
Look closely.
A serious Chinese supplier should provide material certificates, density results, hardness data, dimensional inspection records, and sample approval before mass production. Ask how the factory manages pores, warping, surface cracks, and batch variation. Photographs help, but traceable records help more. Factory experience can reveal practical strengths that a polished catalogue cannot show.
Still, no manufacturer is perfect. I would not trust vague promises, even when the website looks impressive. Buyers should compare drawings, testing methods, packaging details, and response times. A strong partner explains limitations clearly. That honesty may feel less impressive at first, yet it reduces costly surprises later. This guide examines how global buyers can evaluate Chinese tungsten alloy manufacturers through technical capability, quality evidence, production experience, and long-term reliability.
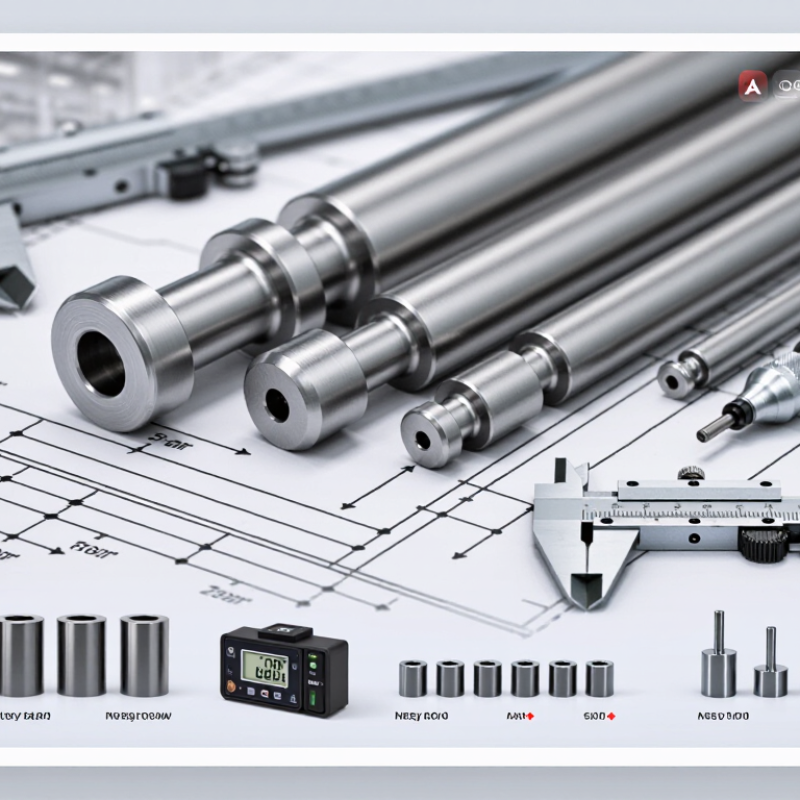
Table of Contents [Hide]
What Defines a Top Tungsten Alloy Manufacturer in China
China Top Tungsten Alloy Manufacturer for Global Buyers?
What Defines a Top Tungsten Alloy Manufacturer in China
A top tungsten alloy manufacturer is defined by controlled metallurgy, not attractive catalogs. Buyers should examine powder selection, alloy composition, density targets, and dimensional tolerances. A capable factory can explain why each parameter matters. It should also provide clear batch records and material traceability.
Production experience becomes visible during pressing, sintering, machining, and final inspection. For example, a dense tungsten heavy alloy component should show consistent weight and stable dimensions across the same batch. Inspection reports should include density, hardness, chemical composition, and surface condition. Records matter. Reliable measurements should come from calibrated equipment and repeatable procedures.
Technical support is equally important for global buyers. Engineers should discuss drawings, operating temperatures, joining methods, packaging, and realistic delivery limits. They should not promise every tolerance without reviewing the application. A supplier that asks precise questions often understands manufacturing risks better. However, no factory is flawless. Occasional variation can still occur, especially with complex shapes or tight machining requirements. Honest communication, corrective-action reports, and sample validation reveal a manufacturer’s real reliability. Buyers may also review quality certifications, export documentation, and independent test results before approving regular production.