-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

Why Choose Tape Applicators for Faster Packaging?
Why Choose Tape Applicators for Faster Packaging?
In busy warehouses, every second at the packing bench matters. Tape Applicators help workers seal cartons with consistent pressure and cleaner alignment. A trained operator can close a box, pull the tape, and cut it in one smooth movement. This reduces repeated hand motions during high-volume packing. It also creates a more uniform appearance across outgoing orders. Small gains become significant when hundreds of cartons move through a line each day.
Practical experience shows that speed is only one part of the decision. The applicator must match the carton size, tape width, adhesive type, and working environment. Lightweight handheld models suit changing order sizes. Bench-mounted units may perform better beside fixed packing stations. Proper tension prevents loose seals, while a sharp cutting blade supports safer, neater work. These details require testing. Not every applicator performs equally well on dusty cardboard or cold packaging areas.
The strongest results come from combining equipment with clear procedures. Workers should check tape adhesion, replace worn blades, and keep rollers free from residue. Simple maintenance matters. It protects consistency and limits avoidable stoppages. Still, no tool solves every packaging problem. Poor carton quality, rushed training, or unsuitable tape can reduce its value. A careful evaluation should measure sealing time, operator comfort, material waste, and long-term reliability. With those factors considered, Tape Applicators can support faster packaging without sacrificing dependable carton closure.
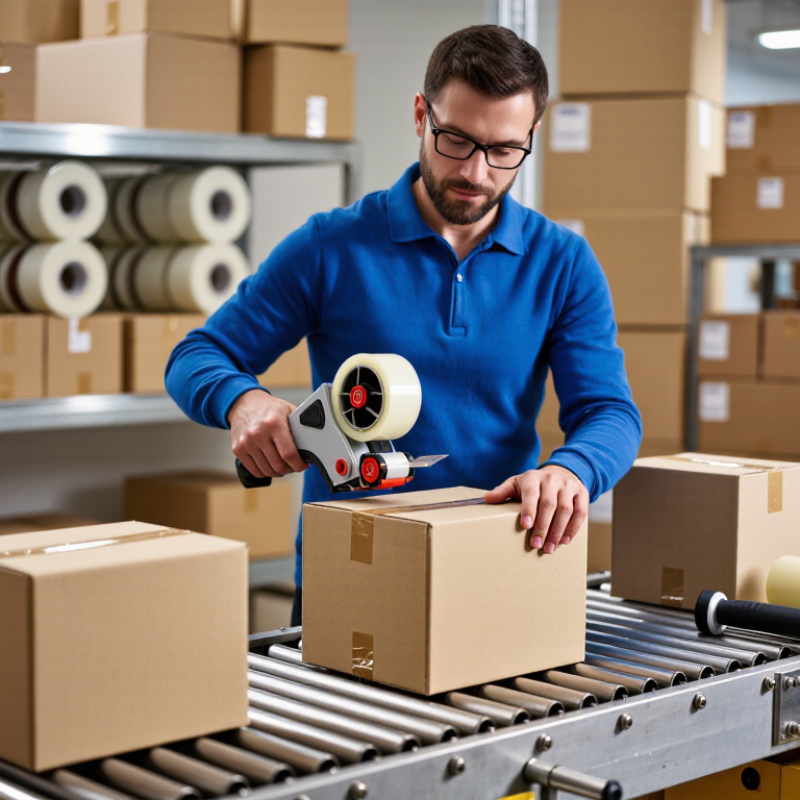
Table of Contents [Hide]
What Are Tape Applicators and How Do They Work?
Tape applicators are machines that place pressure-sensitive tape onto cartons, trays, or bundles. They guide a roll through a tension system, apply the adhesive strip, and cut or wipe it down. Some models use sensors to detect carton length and adjust tape placement automatically. The process is simple. The consistency matters.
In a manual station, an operator may pull tape, align the box, and press the seam by hand. A tape applicator repeats those movements with steadier pressure and fewer pauses. PMMI’s 2023 Packaging Automation report identifies labor availability and productivity as continuing automation drivers. MHI’s 2024 Annual Industry Report also found that 55% of supply-chain professionals viewed workforce shortages as a key challenge. These findings explain the interest in compact, practical automation.
Speed is only part of the decision. A poorly adjusted roller can wrinkle tape, leave open corners, or waste material. That is where real installation experience helps. Operators should test carton sizes, tape width, line speed, and seal strength before full deployment. Measure reject rates, not assumptions. A 2024 Smithers packaging report also highlights efficiency and material reduction as important packaging priorities. Tape applicators can support both goals, but results depend on maintenance and calibration. They are helpful, not magical.
| Packaging Method | How It Works | Typical Throughput | Operator Involvement | Tape Application Quality | Best-Suited Packaging Environment |
|---|---|---|---|---|---|
| Manual taping with loose tape | The operator cuts tape from a roll and applies it directly to the carton by hand. | Approximately 5–10 cartons per minute | High; cutting, positioning, pressing, and sealing are all performed manually. | Variable tape length and alignment; greater risk of wrinkles, loose ends, or missed carton flaps. | Low-volume packing, irregular carton sizes, and occasional shipments. |
| Handheld tape applicator | A spring-loaded or trigger-operated tool dispenses tape, presses it onto the carton, and cuts it with an integrated blade. | Approximately 10–20 cartons per minute | Moderate; the operator guides the tool while the applicator controls dispensing and cutting. | More consistent tape placement and length than loose-hand taping. | Small production lines, fulfillment stations, retail packing, and mixed carton sizes. |
| Gummed-tape applicator | The machine moistens water-activated adhesive tape and applies a measured strip to the carton seam. | Approximately 10–30 cartons per minute | Moderate; the operator feeds or positions the carton and selects the required tape length. | Strong, tamper-evident seals with good adhesion to corrugated fiberboard. | Shipping operations that require secure seals, carton identification, or recyclable paper-based packaging. |
| Semi-automatic case sealer | The operator squares and places the carton into the machine; powered belts transport it while tape is applied to the top and usually the bottom seam. | Approximately 15–30 cartons per minute | Moderate; carton loading and size adjustment are usually required. | Consistent tape position, pressure, and seam coverage when cartons are properly formed. | Repetitive medium-volume packing with relatively standardized carton dimensions. |
| Automatic case sealer | Powered conveyors and forming guides transport, align, and seal cartons with limited manual handling. | Approximately 20–40 cartons per minute | Low during normal operation; staff mainly load cartons, replenish tape, and monitor the line. | Highly repeatable application and consistent carton presentation. | High-volume distribution, manufacturing, and logistics lines using standardized cases. |
| Common pressure-sensitive tape width | Most carton-sealing applicators use a roll mounted on a spindle, with a cutting or wiping mechanism that presses the tape onto the board. | 48–50 mm is widely used; wider formats may be selected for heavier or larger cartons. | Depends on the applicator design and the carton size. | Correct width improves seam coverage and reduces the chance of edge lifting. | General corrugated-carton sealing and dispatch operations. |
| Typical process sequence | Dispense tape → guide or align the carton → press tape onto the seam → cut or wipe the tape end → release the sealed carton. | Fewer manual actions generally increase packing speed and repeatability. | Reduced hand movement can lower operator fatigue during repetitive work. | Controlled tension and consistent pressure help prevent wrinkles and incomplete seals. | Any operation seeking faster, cleaner, and more uniform carton closure. |
| Note: Throughput figures are typical operating ranges for comparison only. Actual results depend on carton dimensions, tape type, operator skill, machine settings, line layout, and the condition of the cartons. | |||||