-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

How to Choose a Pouch Cell Trimming Machine in 2026?
Choosing a Pouch Cell Trimming Machine in 2026 requires more than comparing cutting speed or purchase price. Battery manufacturers now face tighter dimensional tolerances, thinner aluminum laminates, and rising demand for stable production. A suitable machine must trim pouch edges cleanly without exposing the electrode stack or damaging the sealing area. Even a small burr can weaken a seal, create contamination, or increase rejection rates.
Dr. Jeff Dahn, a respected lithium-ion battery researcher, has stated, “Quality is not tested into a battery; it is built into every process step.” This principle applies directly to pouch trimming. Buyers should examine blade alignment, servo control, dust extraction, tooling access, and compatibility with different cell sizes. Ask for measured results, not attractive promises. A practical demonstration should include real pouch material, continuous operation, and inspection of trimmed edges under magnification.
The best Pouch Cell Trimming Machine also supports future production changes. Check whether operators can adjust recipes quickly, replace blades safely, and record key process data. Review service response times, spare-part availability, software support, and training coverage. These details often matter more after installation.
Do not overlook maintenance.
A machine may achieve impressive output during a short trial, yet struggle after weeks of adhesive buildup or blade wear. That concern deserves attention. Some specifications remain incomplete, especially when suppliers avoid publishing tolerance data. Therefore, this guide will compare machine structure, trimming accuracy, automation, safety, lifecycle cost, and supplier reliability. The goal is not to identify the most expensive model. It is to find the machine that produces consistent pouch edges, protects cell quality, and remains manageable on a busy factory floor.
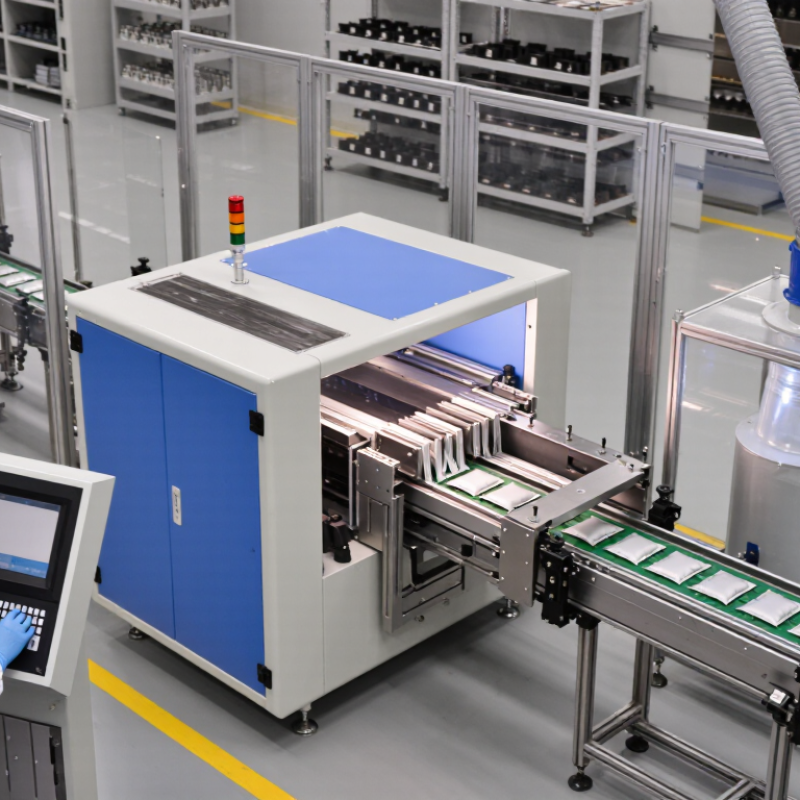
Table of Contents [Hide]
What Is a Pouch Cell Trimming Machine?
A pouch cell trimming machine removes excess aluminum-plastic film after heat sealing. It creates a controlled edge around the cell, keeping later inspection and assembly consistent. The machine usually combines a positioning fixture, cutting tool, sensors, and a collection system. Some models also control trimming depth and record process data. Small details matter.
When choosing one in 2026, start with cell dimensions, film thickness, and required output. A machine for thin film may struggle with thicker structures or frequent format changes. Check edge quality under magnification, not only cycle time. Clean cuts reduce loose particles and improve handling near the sealing area. Ask for sample trials using your actual cells.
Reliable equipment should provide guarded tooling, interlocks, stable clamping, and easy maintenance access. Sensors should detect misplaced cells before the blade moves. Examine changeover time, spare-tool availability, and scrap removal. A fast machine can still be a poor choice if setup errors cause rejects. No machine is perfect. In production, film curl, uneven sealing, and dust can expose weaknesses that showroom tests miss. Leave room for adjustment. Careful records can reveal whether the problem comes from the machine, material, or operator settings.