-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

How to Choose the Best Laser Bending Machine?
Choosing the right Laser Bending Machine can shape your workshop’s productivity, accuracy, and long-term operating costs. The decision is rarely based on laser power alone. Material type, sheet thickness, bending length, production volume, and required tolerances all influence the best choice. A machine that performs beautifully on thin stainless steel may struggle with thicker carbon steel. That difference matters.
Begin with real production needs. Measure your common sheet sizes and record your current bending defects. Watch for uneven angles, edge marks, slow tool changes, or excessive setup time. Servo-driven systems can improve repeatability, while automatic tool changers may reduce labor during varied production runs. However, advanced features are not always valuable. A smaller manufacturer may gain more from reliable controls and accessible maintenance than from an expensive automated package.
Supplier experience deserves equal attention. Ask for sample bends using your own materials, not only polished showroom demonstrations. Examine the finished angle, surface condition, back-gauge movement, and cycle consistency. Request clear information about training, spare parts, software updates, warranty coverage, and service response times. These details often become more important after installation.
Do not ignore safety.
Review guarding, emergency controls, operator visibility, and training procedures with qualified professionals. Energy consumption and floor space also affect the true purchase cost. I have seen buyers focus on maximum capacity, then discover that their daily work rarely needs it. That is an expensive lesson. A careful comparison, supported by production data and independent technical advice, can lead to a Laser Bending Machine that remains practical, accurate, and dependable for years.
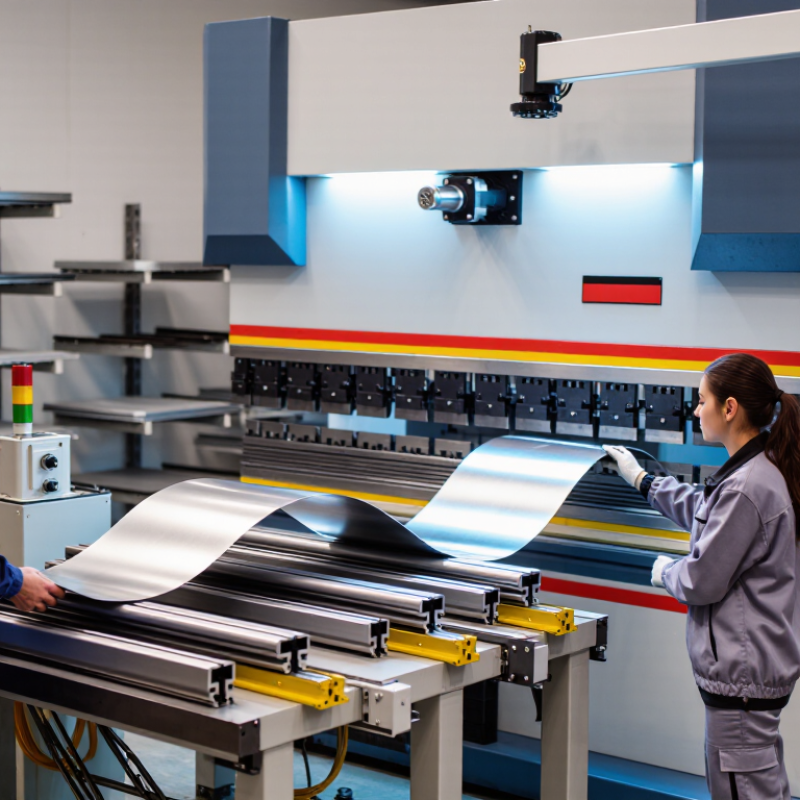
Table of Contents [Hide]
What Is a Laser Bending Machine and How Does It Work?
A laser bending machine uses a focused laser beam to shape metal without traditional dies. The beam heats a narrow line on the workpiece. Thermal expansion is restricted by the cooler surrounding metal. As the heated area cools, the material contracts and bends along the scanned path.
The process depends on power, beam diameter, travel speed, and material thickness. A CNC system controls the laser movement and bending angle. Sensors can monitor temperature and position, reducing variation between parts. In practical workshops, steel, stainless steel, and some aluminum alloys respond differently. Therefore, test samples matter. A setting that works well on one sheet may distort another.
When choosing a machine, check its laser power range, motion accuracy, cooling system, and software controls. Ask whether it supports your actual materials and target angles. A reliable supplier should provide process data, maintenance guidance, and operator training. Look for safety enclosures, interlocks, and clear emergency controls. Small details matter.
The first trial is rarely perfect. Slight springback may remain after cooling. Operators often adjust scanning speed or repeat the heating path carefully. Excessive heat can discolor the surface or weaken a sensitive area. For this reason, the best machine is not always the most powerful one. It should offer stable control, repeatable results, and practical adjustment for your production needs.