-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint







How to Choose the Right Bus Handrail for Global Sourcing
Choosing the right Bus Handrail for global sourcing is not merely a matter of selecting a polished metal tube. It affects passenger stability, vehicle safety, installation speed, and long-term maintenance. A suitable handrail should feel secure in a crowded aisle, even when the bus turns sharply or stops suddenly. As transit ergonomics expert Dr. John J. Fruin noted, “The handrail is a critical element in maintaining passenger stability.” This principle remains practical today.
A reliable sourcing process begins with the operating environment. City buses may face rain, humidity, road salt, dust, or extreme temperature changes. Stainless steel can resist corrosion, while powder-coated aluminum may reduce weight. However, material choice alone does not prove quality. Check the tube diameter, wall thickness, surface smoothness, mounting strength, and grip comfort. A 32-millimeter diameter often suits adult passengers, but actual user testing remains valuable. Children, older adults, and passengers wearing gloves may experience the product differently.
Supplier evaluation also requires physical evidence. Request samples, load-test records, dimensional drawings, surface-finish details, and traceable material documents. Inspect welded joints closely. Small rough edges can become uncomfortable after thousands of daily contacts. Confirm packaging quality, replacement availability, and communication during production. Global sourcing sounds efficient. It can also hide weak assumptions. A supplier may meet the drawing but miss the passenger experience. Another may offer a low price while creating costly installation delays. The best decision balances safety, ergonomics, durability, compliance, and total lifecycle cost. Some choices will remain imperfect, so record the reasoning and review it after field use.
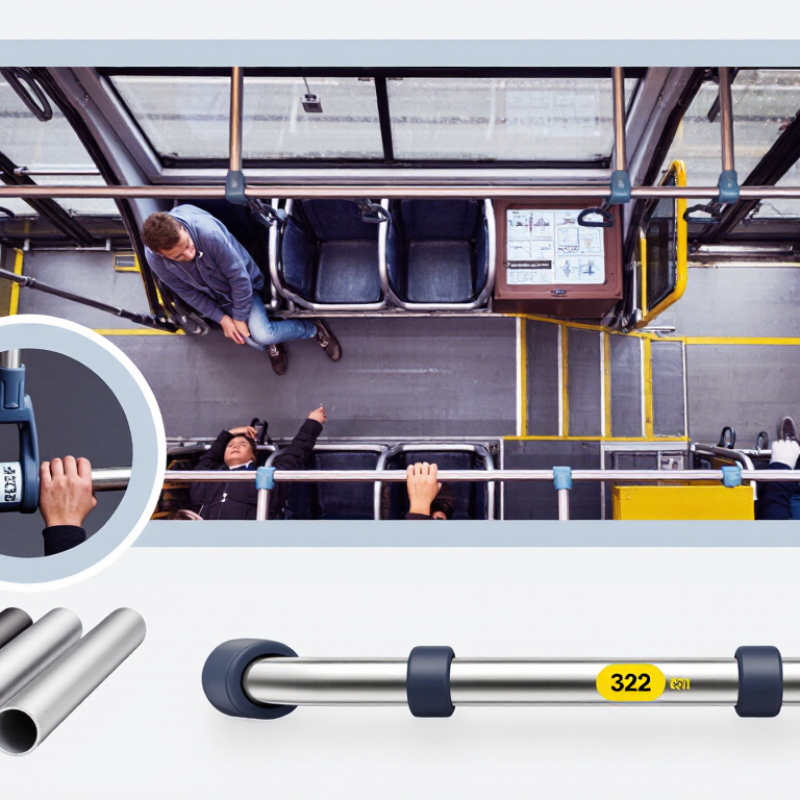
Table of Contents [Hide]
Define Grip Geometry with ADA’s 32–51 mm Diameter and 38 mm Clearance
How to Choose the Right Bus Handrail for Global Sourcing
Grip geometry should be defined before comparing suppliers. The U.S. Access Board’s ADA 2010 Standards specify a circular handrail diameter of 32–51 mm. They also require at least 38 mm of clearance between the rail and adjacent surfaces. These measurements support secure gripping, especially for passengers with limited hand strength. A 40 mm tube often feels balanced, but passenger feedback may challenge that assumption.
For global sourcing, place these dimensions directly on the technical drawing. Specify finished diameter, not only tube diameter. Powder coating, rubber sleeves, and weld seams can change the final grip. Use a calibrated caliper during inspection. Also check the 38 mm clearance near brackets, windows, and seat backs. The Transit Cooperative Research Program highlights frequent contact and high passenger turnover in bus interiors, making surface durability and cleanability practical purchasing concerns. ADA remains a useful benchmark, not a universal global requirement. Local accessibility rules still need verification.
Tips: Request first-article samples from each supplier. Test them with wet and gloved hands. Measure the coated rail at several points. Do not trust one reading. A small tolerance error can reduce clearance or create an uncomfortable grip. Include a drawing revision number, inspection method, and acceptance range in every purchase order.