-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

How to Choose a Steel Pipe Making Machine?
Choosing a Steel Pipe Making Machine is not simply a question of production speed. The right line must match your pipe dimensions, steel grades, expected output, and available floor space. A machine built for thin-wall tubing may not suit heavy-wall pipe, even when both products look similar in a catalog. Define your product range clearly: outer diameter, wall thickness, pipe length, and required tolerances. Be specific.
The forming method, welding process, and sizing system affect both product quality and operating costs. Check whether the machine can handle your planned material thickness and whether changing rolls between sizes is practical. Ask about line speed under real production conditions, not only the maximum listed in a brochure. Details matter. Review the controls, cutting equipment, safety features, power needs, and maintenance access. A crowded layout can make routine servicing harder than expected. Ask the supplier for references, sample pipes, technical drawings, and a factory acceptance test plan. Confirm what installation, operator training, spare parts, and after-sales support include. Compare total ownership costs, including tooling, energy, and downtime, rather than purchase price alone. No machine is perfect. Some specifications may need compromise, and that deserves honest discussion before ordering. A careful comparison helps you choose equipment that fits actual production needs, instead of paying for capacity or features your operation may not use.
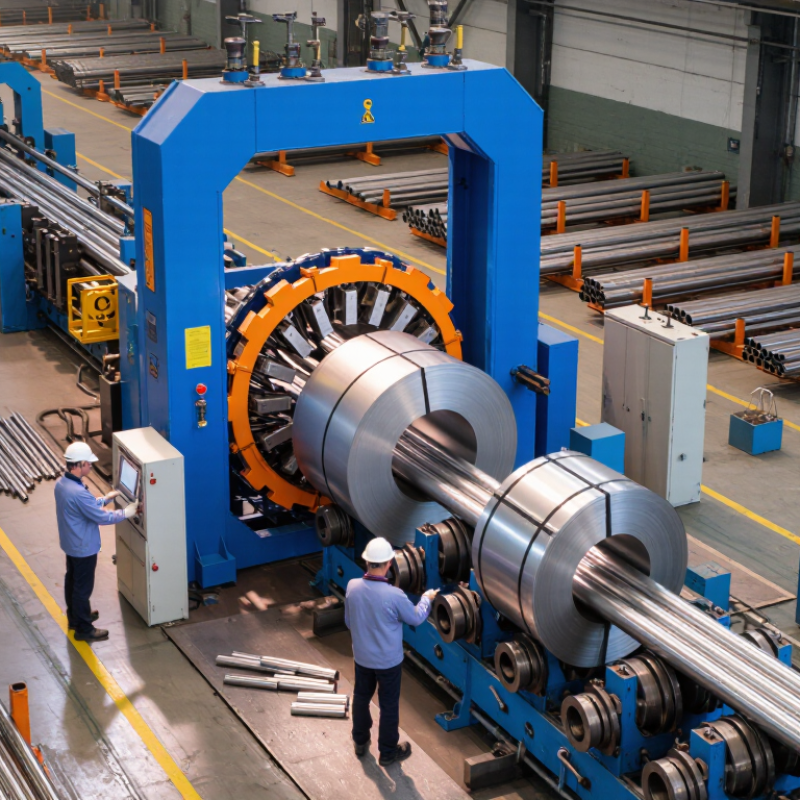
Table of Contents [Hide]
Define Pipe Requirements: ASTM A53 Covers NPS 1/8–26
Before choosing a steel pipe making machine, define the required size range, wall thickness, grade, and production method. ASTM A53/A53M covers pipe from NPS 1/8 through NPS 26, but NPS is a nominal designation, not the measured outside diameter. ASME B36.10M lists an outside diameter of 0.405 inches for NPS 1/8 and 26 inches for NPS 26. That is a substantial forming range. Not a small adjustment.
These dimensions affect forming rolls, sizing stands, tooling changes, and line layout. For example, a machine set up for small-diameter pipe may not accommodate the tooling or forming loads required for larger pipe. Wall thickness matters too: confirm the schedules and tolerances needed for your orders against the relevant ASTM requirements. Standards define the product; they do not guarantee that one mill configuration can efficiently produce every size.
Ask suppliers for a documented size-and-thickness matrix, then compare it with your target products and ASTM A53 pipe type. Check changeover time and trial-run records, not just maximum capacity. Measure twice. I would also leave room for uncertainty: published capacity figures can depend on material grade, wall thickness, and operating speed. Verify those assumptions using the same product specification you plan to manufacture.