-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint







2026 Top Aluminium Tri Fold Blind Rivets for Composites
Choosing the right fastener for composite panels is rarely a simple catalogue decision. Aluminium Tri-Fold Blind Rivets For Composite Materials offer broad load distribution behind fragile skins. Their three-legged expansion can reduce pull-through risk when access is available from one side only. This matters in sandwich panels, fiberglass enclosures, lightweight vehicle bodies, and interior structures.
Composite fastening specialist Dr. Stephen W. Tsai has emphasized, “Composite design is not simply metal design with different materials.” That principle guides this 2026 review. Rivet selection must consider laminate thickness, core density, hole quality, grip range, and washer support. Aluminium provides low weight and useful corrosion resistance. However, it may not suit every galvanic environment. Sealants, coatings, and isolation layers can change the result.
Small details matter.
A clean hole protects the laminate. Correct clamping prevents crushing. Controlled installation reduces uneven expansion. The rivet should fill the hole without forcing excessive pressure into the panel. Laboratory data helps, but field conditions can be less polite. Temperature changes, vibration, moisture, and hidden voids may weaken an otherwise attractive joint. That is the uncomfortable part.
This guide compares leading aluminium tri-fold blind rivets for 2026 applications. It considers practical installation, head design, mandrel retention, corrosion behavior, and composite compatibility. Readers should still validate every choice through representative testing. No chart can replace a real trial. Even experienced engineers occasionally overlook washer placement or local skin damage. Careful inspection remains essential, especially where repair access is limited and failure would be costly.
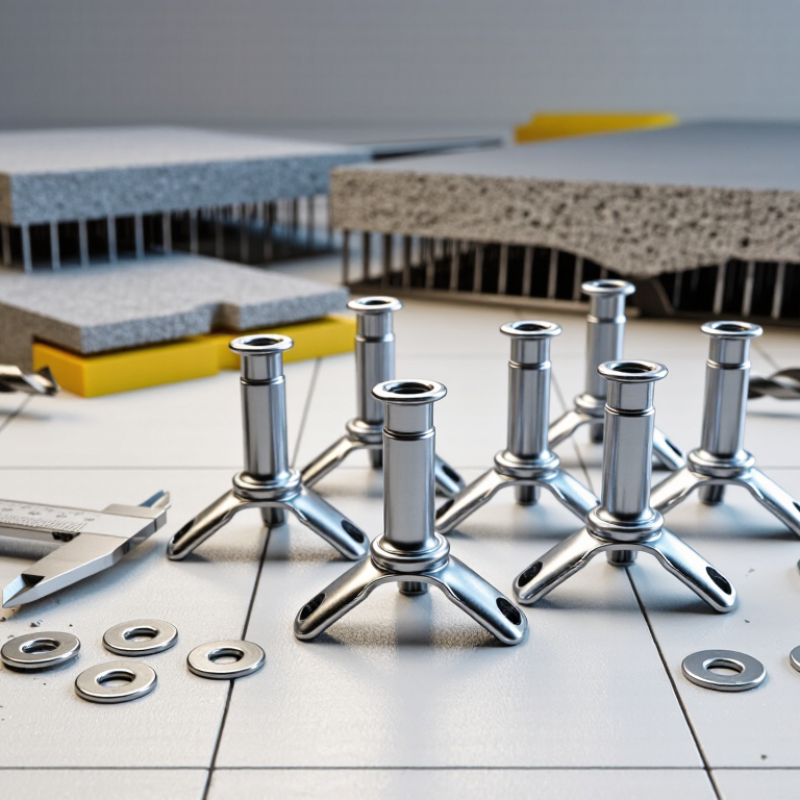
Table of Contents [Hide]
What Are Aluminium Tri-Fold Blind Rivets for Composite Materials?
Aluminium tri-fold blind rivets are fasteners designed for joining composite materials where access is available from one side. Their body expands into three broad legs behind the panel. This action spreads clamping pressure over a larger area than a standard blind rivet. It can reduce pull-through risks in thin laminates, honeycomb panels, and molded composite covers.
The aluminium body is lightweight and resists many forms of corrosion. However, it may not suit every environment. Contact with carbon-fiber composites can create galvanic corrosion when moisture enters the joint. A compatible coating, isolating washer, or barrier layer may be necessary. Hole accuracy also matters. Oversized holes can reduce grip, while excessive tightening may crush the laminate. In field repairs, technicians should inspect the panel thickness, rivet grip range, and rear-side expansion before installation. Small errors become expensive later.
Tips: Use a sharp, properly sized drill, and remove loose fibers around the hole. Choose a rivet with enough expansion space behind the panel. Test one fastener on scrap material first. This simple step often reveals unexpected crushing or poor setting. Do not judge strength by appearance alone. Check the joint under realistic vibration and load conditions, because composite behavior can be less predictable than metal.