-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

China Top 304 Stainless Steel Plate Suppliers?
Finding reliable China Top 304 Stainless Steel Plate Suppliers requires more than comparing prices. Buyers should examine production experience, material traceability, and export performance. A supplier may offer attractive quotations, yet inconsistent thickness can create serious problems during fabrication. The best companies usually provide clear specifications, mill test certificates, and responsive technical support.
This guide introduces practical ways to evaluate 304 Stainless Steel Plate manufacturers in China. It considers product quality, manufacturing capacity, surface finishes, dimensional accuracy, and international standards. Common references include ASTM, ASME, EN, and JIS requirements. Buyers should also confirm whether plates are hot rolled, cold rolled, polished, or cut to custom dimensions. Small details matter. A clean No. 4 finish should look uniform under direct warehouse lighting, without visible scratches or uneven polishing marks.
Supplier verification should include factory audits, sample testing, and documented inspection procedures. Experienced exporters can explain lead times, packaging methods, loading conditions, and corrosion resistance in real applications. However, no supplier should be trusted solely because of a polished website or a low initial offer. That assumption is risky. Independent testing may reveal differences in chemical composition, hardness, or surface quality.
The selection process is not perfectly simple. Even reputable suppliers can face delays, communication gaps, or production variations. This guide therefore encourages careful comparison rather than automatic ranking. It focuses on evidence, practical experience, and transparent communication. With the right questions, buyers can identify dependable Chinese suppliers and reduce costly surprises before placing a large order.
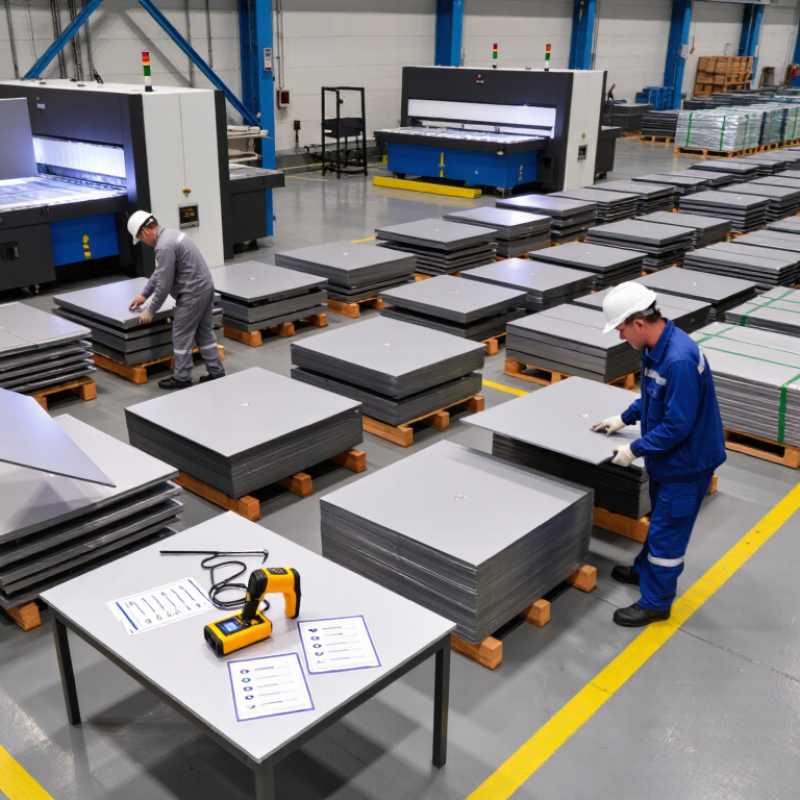
Table of Contents [Hide]
304 Stainless Steel Plate: Properties, Grades, and Common Applications
China Top 304 Stainless Steel Plate Suppliers?
304 stainless steel plate remains a practical choice for many industrial projects. It typically contains about 18% chromium and 8% nickel. This chemistry supports corrosion resistance, cleanability, and good forming performance. ASTM A240 commonly specifies minimum tensile strength near 515 MPa and yield strength near 205 MPa for Type 304 plate. Actual values depend on thickness, processing, and testing conditions.
There are useful grade differences. Standard 304 suits tanks, kitchen equipment, architectural panels, and general fabrication. 304L contains less carbon, reducing the risk of weld-related corrosion. 304H contains higher carbon and may support elevated-temperature service. EN 10088-2 and ASTM A240 provide widely used requirements, but buyers should verify the exact edition and mechanical values. A mill certificate matters. Surface appearance alone proves very little.
World Stainless reported approximately 58.4 million tonnes of global stainless crude steel production in 2023. That scale reflects strong demand, yet volume does not guarantee plate quality. Chinese suppliers should provide heat numbers, chemical analysis, dimensional inspection, and traceability records. I would also check flatness, edge condition, and surface finish under real lighting. Bright plate can hide scratches. It can happen. For chloride exposure or severe chemical service, 304 may be an optimistic selection; testing and engineering review should guide the final grade.