-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

Who Are the Top CNC Metal Parts Manufacturers in China?
China has a broad network of manufacturers producing precision components for industrial equipment, electronics, automotive systems, and medical devices. Yet finding a dependable partner takes more than comparing prices or polished website photos. Buyers need to understand a factory’s machining capabilities, material options, inspection methods, and communication practices. Small details matter. A cleanly machined aluminum housing, for example, may still fail if its threaded holes or surface finish miss the drawing requirements.
This guide to the top Cnc Metal Parts manufacturers in China examines what separates capable suppliers from merely convenient ones. It considers equipment and processes such as CNC milling, turning, multi-axis machining, and finishing, alongside evidence of quality control. Look for documented inspection procedures, clear tolerance discussions, and sample parts that match the intended application. Ask how the supplier handles drawing revisions and production issues, too. Those conversations can reveal more than a catalog.
There is no single best manufacturer for every project. A workshop suited to short runs may not be ideal for large-volume production, while a low quote may omit packaging, finishing, or inspection costs. Supplier rankings can also change as capabilities and customer needs evolve. Treat any shortlist as a starting point, then verify claims through technical discussions, references, and sample evaluation. The right Cnc Metal Parts partner should make requirements clear and flag risks early. Even experienced buyers can miss something. Check twice.
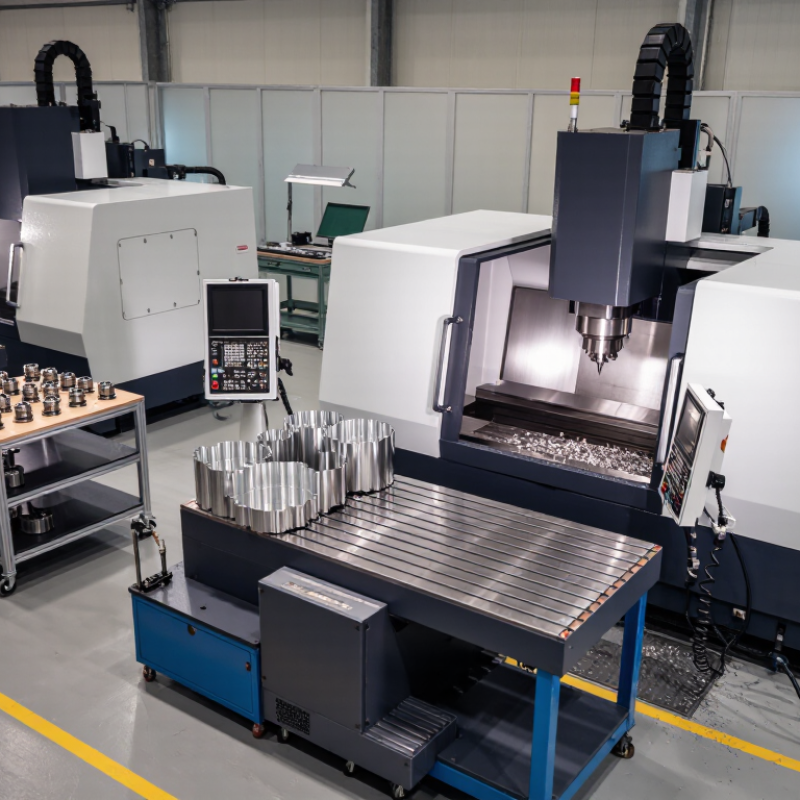
Table of Contents [Hide]
What Makes a CNC Metal Parts Manufacturer a Leader in China?
A leading CNC metal parts manufacturer in China is not defined by machine count alone. It must turn drawings into parts that fit, function, and arrive consistently. Engineers should review tolerances, material grades, surface finishes, and production quantities before quoting. That early discussion can reveal design risks, such as a deep pocket that needs special tooling. Small details matter.
Strong manufacturers use documented processes for machining, deburring, and inspection. They can explain how they measure critical features, using tools such as micrometers or coordinate measuring machines when appropriate. Ask for sample parts and inspection records for features that affect fit. Reliable suppliers also track material batches and communicate changes promptly. A polished website is not proof. Real capability shows in repeatable results and clear answers. Even capable teams can miss a detail, so review drawings together.
Tips: Send a fully dimensioned drawing and identify critical tolerances. Request a sample run before larger orders. Compare inspection reports, lead times, and communication—not just unit price. Ask how the supplier handles a part that fails inspection.