-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint

Top Machining Parts Manufacturers for Global Buyers?
Choosing the right Machining Parts manufacturer can determine whether a project stays reliable, profitable, and on schedule. Global buyers often compare prices first, yet cost alone reveals little about production discipline. A supplier may offer attractive quotations while lacking stable tolerances, material traceability, or dependable communication.
Experienced buyers inspect more than catalogs. They review equipment lists, inspection methods, certifications, and previous export experience. A serious manufacturer should explain its CNC capabilities, surface treatments, quality controls, and packaging procedures clearly. Ask how the supplier handles a drawing revision or a failed inspection. The answer often shows more than a polished website.
Small details matter. A machined aluminum housing should arrive with clean threads, protected surfaces, and measured dimensions. Stainless steel components require suitable tooling and careful control of heat. Reliable suppliers document these steps through inspection reports, material certificates, and sampling records. They also understand international shipping requirements and communicate realistic lead times.
No supplier is flawless. That matters. Even experienced factories can face machine maintenance, material delays, or unclear specifications. The stronger partners report problems early and propose practical corrections. Buyers should still verify claims independently, request samples, and define acceptance standards before production begins.
This guide examines leading Machining Parts manufacturers for global buyers. It considers technical capacity, quality assurance, communication, pricing transparency, and long-term reliability. The goal is not to praise the largest company automatically. It is to identify manufacturers that can turn accurate drawings into consistent components, shipment after shipment.
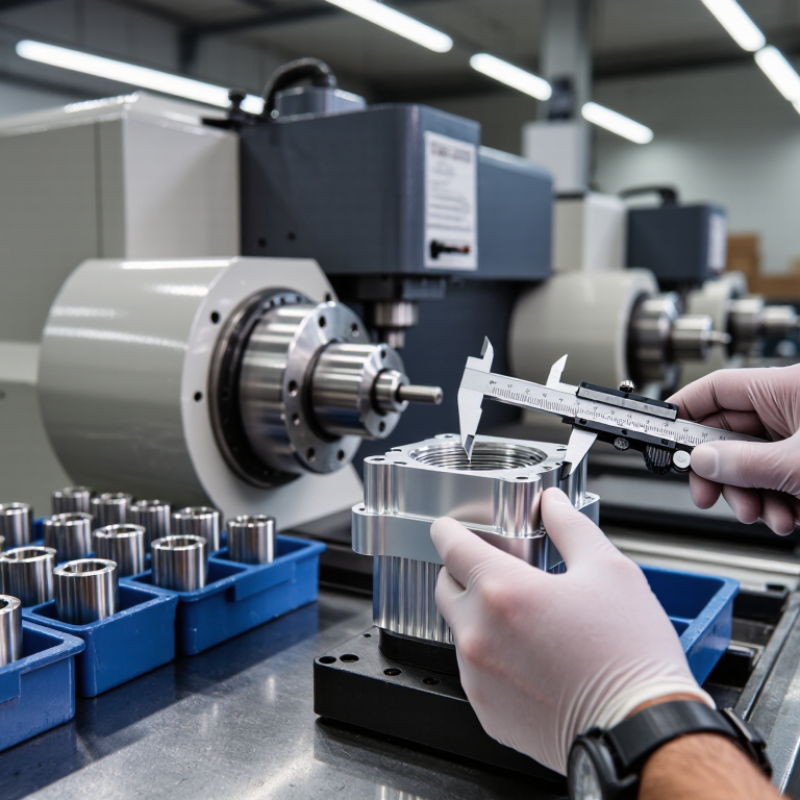
Table of Contents [Hide]
What Defines a Leading Machining Parts Manufacturer
Top Machining Parts Manufacturers for Global Buyers?
What Defines a Leading Machining Parts Manufacturer
A leading machining parts manufacturer earns trust through repeatable results, not polished promises. In practical sourcing, buyers should inspect process capability, inspection records, and communication habits. A stable facility can explain its tolerances, materials, and surface finish limits clearly. It should also provide sample reports with measured dimensions, datum references, and equipment details. Vague answers often become expensive delays. That matters.
Technical strength appears in the details. Experienced engineers review drawings before production and identify thin walls, deep bores, or difficult tool paths. They may suggest a safer radius or revised tolerance when the design allows it. This protects the customer’s intent while reducing chatter, distortion, and rework. Reliable manufacturers control cutting parameters, tool life, coolant condition, and inspection frequency. Their quality system should support traceability from material certificates to final packing. Calibrated instruments and trained inspectors provide stronger evidence than attractive factory photographs.
However, capability claims deserve testing. A supplier may show impressive machinery yet struggle with a small pilot order. Requesting a prototype, first-article report, and corrective-action process exposes gaps early. Delivery history matters too, but one late shipment should not define an entire partnership. Buyers should examine the cause, response, and prevention plan. No workshop is perfect. Even a strong manufacturer can miss details when drawings, revisions, or inspection criteria remain unclear. The best partners admit that risk, ask precise questions, and document decisions before production begins.