-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint







Top Peel Tensile Testing Machines for Global Buyers
Global packaging, labeling, electronics, and medical-device manufacturers increasingly depend on controlled adhesion data. MarketsandMarkets identifies packaging testing as a growing sector, driven by flexible formats, automation, and stricter quality expectations. Smithers also reports continued investment in packaging performance, especially for lightweight films and recyclable structures. These trends make a reliable Peel Tensile Testing Machine more than a laboratory purchase. It becomes a safeguard against weak seals, inconsistent laminates, and costly product returns.
A suitable machine applies steady peel force while recording load, distance, and failure behavior. ASTM D3330, ASTM F88, and ISO 8510-2 provide useful reference methods, depending on the material and test purpose. Results still depend on specimen width, peel angle, speed, conditioning, and operator technique. Small differences matter. A film may separate cleanly at 23°C, then tear irregularly after humidity exposure. That detail can change a purchasing decision.
Adhesion specialist Dr. George Wypych offers a practical principle: “Adhesion must be evaluated under conditions that represent its intended use.” Buyers should treat that warning seriously. A high peak value alone does not prove dependable performance. Repeatability, calibration records, software traceability, and fixture quality deserve equal attention. In practice, some procurement teams overvalue maximum force and overlook failure mode. That is an avoidable weakness. The best Peel Tensile Testing Machine supports comparable data across laboratories, suppliers, and production shifts. Yet no instrument removes judgment entirely. Test methods must be reviewed, challenged, and improved as materials change.
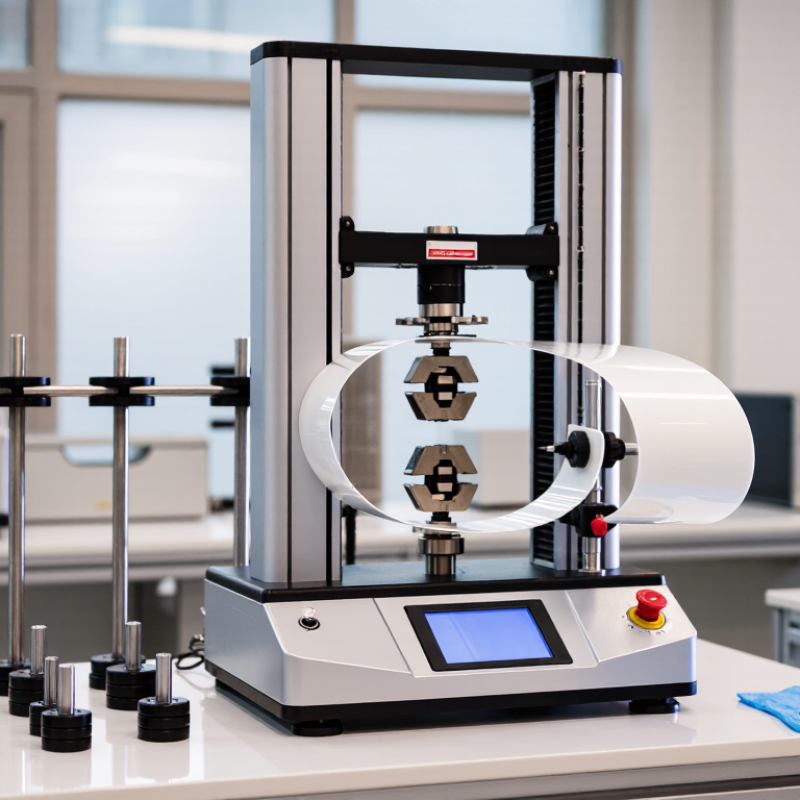
Table of Contents [Hide]
What Is Peel Tensile Testing and Why Does It Matter?
Peel tensile testing measures the force required to separate two bonded materials. In packaging, the test often uses a controlled 90° or 180° peel angle. Results are reported in newtons per 15 millimetres or a similar unit. ASTM D1876 and ISO 8510-1 provide widely used methods for evaluating flexible bonded materials.
The test reveals whether a seal opens smoothly, tears unpredictably, or fails inside the adhesive layer. This matters for pouches, medical packaging, labels, and laminated films. Eurostat reported 186.5 kilograms of packaging waste per person in the European Union during 2022. Reliable seals can reduce leakage, rejected batches, and unnecessary material loss. Small force changes can expose coating variation, weak curing, or uneven pressure during production.
A strong result is not automatically a safe result. Excessive peel strength may make opening difficult for users. A low result may still be acceptable for a deliberately easy-open package.
Testing should match the real product, including temperature, humidity, sealing speed, and storage time. ASTM committee guidance also stresses conditioning because environmental exposure can alter adhesive performance. Laboratory strips are clean; factory materials are not. That gap deserves attention. Global buyers should request test speed, specimen width, conditioning details, failure mode, and repeatability data before comparing machines. A precise instrument cannot repair a poorly designed test.