-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint







Top 10 Types of Thermoforming Machines for Global Buyers
Choosing the right Thermoforming Machine is rarely a simple purchase decision. Global buyers must compare forming methods, material compatibility, output speed, tooling costs, and after-sales support. A machine that performs well in a high-volume packaging plant may struggle in a smaller workshop with limited floor space. Real operating conditions matter.
This guide examines ten major types of thermoforming machines used across packaging, medical, food, automotive, and consumer-product manufacturing. Each type offers a different balance between automation, precision, energy use, and production flexibility. Rotary systems can support continuous output, while inline machines often suit integrated production lines. Vacuum forming remains practical for selected shapes, but pressure forming may deliver sharper details and cleaner surfaces.
Look closely.
Reliable selection also requires attention to heating zones, mold-change time, sheet thickness, cooling capacity, and control systems. Buyers should request production samples, inspect safety features, and verify service response in their region. Supplier claims can sound impressive. Factory evidence is stronger.
This overview follows practical purchasing experience and established manufacturing principles, while recognizing that specifications vary by supplier and application. No single machine fits every factory. That assumption often creates avoidable costs. The final decision should consider current demand, future expansion, trained operators, maintenance access, and the materials approved for the finished product. Some recommendations may need revision after testing, because actual forming results can differ from catalog data.
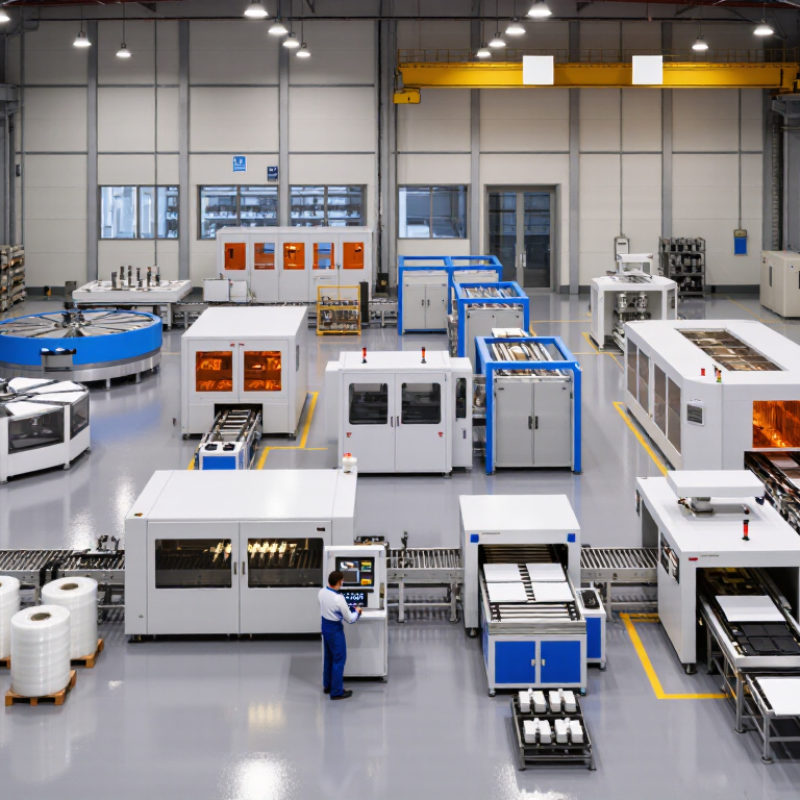
Table of Contents [Hide]
What Thermoforming Machines Are and How They Are Classified
Thermoforming machines heat plastic sheets until they become flexible. A mold then shapes the softened sheet through vacuum, air pressure, or mechanical force. Cooling fixes the final form. Trimming usually follows. Unlike injection molding, thermoforming starts with a sheet, so heating control and material distribution are critical. In practical purchasing work, the machine must match the product, material, output, and available floor space.
The ten common categories include vacuum, pressure, twin-sheet, plug-assist, roll-fed, cut-sheet, inline, rotary, single-station, and continuous thermoformers. Vacuum machines pull heated plastic against a mold and suit many simple shapes. Pressure systems add compressed air for sharper details. Twin-sheet machines form two parts and join them into hollow products. Plug-assist units improve wall thickness in deep cavities.
Roll-fed systems support steady production, while cut-sheet models offer flexible batch handling. Inline, rotary, and continuous machines target higher throughput. Single-station equipment suits prototypes, short runs, and changing molds.
This classification is useful, but it is not perfectly rigid. One machine may combine several operating methods. Engineers also examine heating zones, mold cooling, forming depth, trim accuracy, and scrap handling. Material thickness can change cycle time more than expected. A small sample run often exposes weak corners, uneven walls, or difficult release angles. Specifications alone can mislead. I would not choose a machine from output numbers only; real parts, tooling trials, operator skill, and maintenance access deserve equal attention.