-
PRODUCTS & SERVICESOptimized cooling solutions for modern data centersProducts & ServicesOptimized cooling solutions for modern data centers
-
CAPABILITIESAdvancing liquid cooling technologiesCapabilitiesAdvancing liquid cooling technologies
-
TechnologiesLiquid Cooling InnovationTechnologiesLiquid Cooling Innovation
-
RESOURCESLatest News & InformationResourcesLatest News & Information
-
ABOUTOur history, leadership and ownershipAboutOur history, leadership and ownership
-
CONTACTFacility locations and global operational footprint







Why Choose a CNC Vertical Turning Lathe?
Choosing a Cnc Vertical Turning Lathe begins with understanding the workpiece, not admiring the machine.
Large, heavy components often need stable support during turning. A vertical design places the spindle above the work area. Gravity helps keep the workpiece seated on the table. This matters when machining gears, flanges, rings, turbine parts, and bearing housings.
The setup feels different.
Operators can load a wide component with a crane. They can inspect the cutting zone more directly. A rigid column and short tool path may also reduce vibration during roughing. That advantage becomes visible when a carbide insert removes several millimeters of steel.
Frederick Winslow Taylor, a pioneer in machining and industrial engineering, wrote, “In the past man has been first. In the future the system must be first.” His statement remains useful here. A CNC Vertical Turning Lathe should serve the entire production system, including fixtures, tooling, inspection, programming, and operator training.
Manufacturers should compare spindle torque, table diameter, axis travel, tool capacity, and control functions. They should also examine chip evacuation and service support. A powerful spindle cannot rescue a weak fixture. A precise machine cannot correct poor measurement practice.
Real production is less perfect.
A machine may promise tight tolerances, yet heat, tool wear, and uneven castings still influence results. Trial cuts and process records remain valuable. Engineers should question optimistic cycle-time claims. Sometimes, a simpler Cnc Vertical Turning Lathe produces more reliable parts than a heavily equipped model.
The best choice balances capacity, repeatability, accessibility, and long-term maintenance. It is not merely a purchase. It is a commitment to controlled machining.
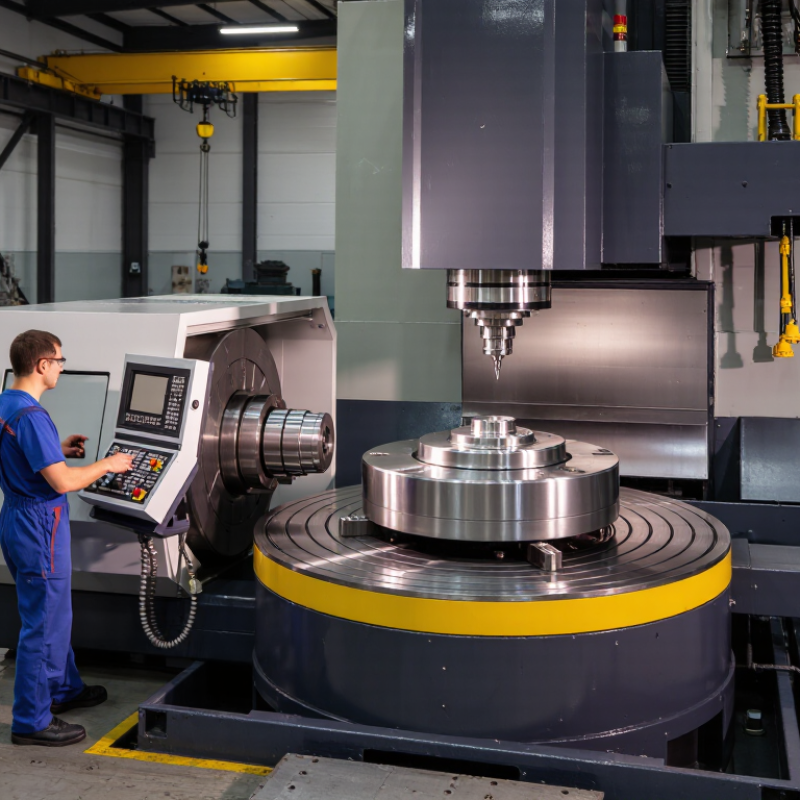
Table of Contents [Hide]
What Is a CNC Vertical Turning Lathe?
What is a CNC vertical turning lathe? It is a computer-controlled machine with a vertical spindle axis. The workpiece sits on a rotating table or chuck. Cutting tools move across its face, diameter, and internal surfaces. Gravity helps support heavy, wide components during loading. This layout suits rings, flanges, gears, and large bearing housings.
The design is not merely a taller turning machine. Its rigid structure can reduce deflection when tools cut deep or uneven surfaces. Operators can program spindle speed, feed rate, tool movement, and machining cycles. According to Fortune Business Insights’ CNC Machine Market report, the global CNC machine market was valued at about USD 83.8 billion in 2023. The report also forecasts continued growth through 2032, driven partly by automation and precision manufacturing.
In a workshop, the difference becomes visible quickly. A crane places a broad steel blank onto the table. The jaws clamp it, and the probe checks its position before cutting begins. That workflow can improve repeatability and reduce manual alignment time. However, CNC does not remove every problem. Thermal drift, worn inserts, poor clamping, and incorrect programs still create scrap. The word “automatic” can mislead. According to the International Federation of Robotics’ World Robotics 2023 report, global industrial robot installations reached 553,052 units in 2022, showing wider automation growth. Yet skilled setup remains essential, especially for oversized parts and demanding tolerances.